
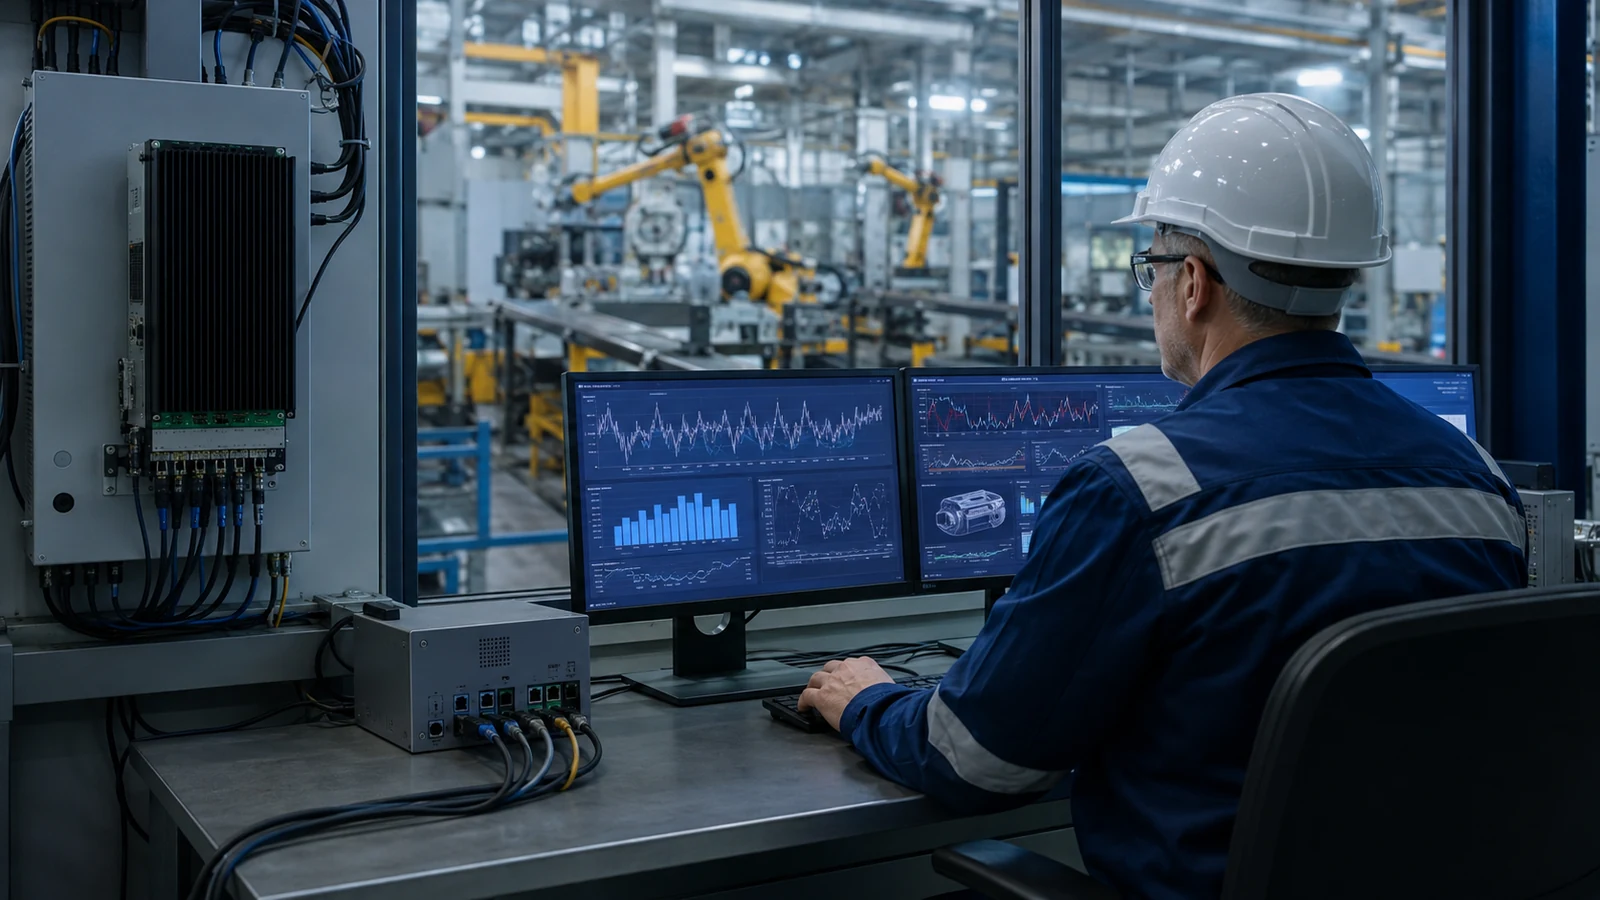
An industrial IoT implementation connects physical production assets to a data and decision system. The useful starting point is not a platform purchase. It is one measurable production loss, one group of assets and one decision that better data could improve. A manufacturer should then build the smallest secure data path that can test whether the decision creates enough value.
This approach changes the budget. Sensors and software matter, but they are rarely the complete cost. Legacy interfaces, data context, engineering time, cybersecurity, commissioning and long-term support can consume more money than expected. A credible business case therefore prices the full operating model, not a list of devices.
What does an industrial IoT implementation include
A complete IIoT implementation includes data acquisition, communication, contextualization, applications, enterprise integration, cybersecurity and ongoing ownership. If one of these layers is missing, connected machines may produce data without producing a reliable decision.
At the asset layer, data comes from existing PLCs, machine controllers, drives, meters, sensors or retrofit devices. The first task is an inventory. The team needs to know which assets can expose data, which protocols they use, how frequently values change and whether reading a tag could affect a validated control system. A retrofit sensor may be appropriate when a controller is closed or obsolete, but it can also create a second version of the truth.
The edge layer collects, filters and sometimes analyzes data near the process. An industrial gateway may translate protocols, buffer records during a network interruption and calculate simple features. Local processing is important when latency is short, connectivity is unreliable or sending raw high-frequency data would be wasteful.
The platform layer stores and organizes information. Raw tags need context: asset identity, product, order, shift, recipe, operating state and unit of measure. A temperature value without a timestamp, sensor location and production state is not ready for analysis. This semantic work is easy to omit from an equipment quotation and expensive to repair after hundreds of tags have been connected.
The application layer turns data into an action. It may show a condition alert, calculate energy per good unit, detect a process drift or provide evidence for a maintenance decision. Finally, the enterprise layer exchanges selected information with MES, ERP, QMS or maintenance systems. The objective is not to copy every tag into every application. It is to place the right fact in the workflow where a person or system can act on it.
The Industrial Internet Reference Architecture describes these concerns through functional domains and system viewpoints. The OPC UA overview explains how a common information model and communication services can support interoperability from devices to enterprise applications.
How much does industrial IoT cost
There is no reliable universal price for industrial IoT. Cost depends on the number and age of assets, protocol diversity, sampling rate, data retention, integration scope, security controls, availability requirements and the amount of internal engineering work.
A quote for sensors and a cloud subscription can therefore understate the investment. The budget should distinguish one-time implementation cost from recurring operating cost and from internal time that does not appear on a supplier invoice.
| Cost component | Main cost driver | Timing | Common omission |
|---|---|---|---|
| Sensors and retrofit hardware | Number of assets, environment, accuracy and certification | One time, with replacement | Mounting, calibration and cabling |
| Gateways and industrial network | Protocols, segmentation, redundancy and distance | One time plus support | Switches, cabinets and network engineering |
| Data integration | PLC access, tag quality, connectors and legacy documentation | Mainly one time | Reverse engineering undocumented machines |
| Data platform and storage | Volume, frequency, retention, users and service level | Recurring | Test environments, backups and data egress |
| Applications and analytics | Number of use cases and model complexity | One time plus updates | Validation and false-alert handling |
| Cybersecurity | Zones, conduits, identity, monitoring and incident response | One time and recurring | Patch ownership and supplier remote access |
| Commissioning and training | Production access, shifts and acceptance tests | One time | Lost output during installation and testing |
| Internal labor | Operations, controls, IT, security and maintenance hours | One time and recurring | Time spent cleaning tags and resolving exceptions |
A reviewed case study of an HVAC production line reported about USD 30,000 for hardware and software. It also reported roughly 8,500 hours from eight IT specialists, 2,500 hours during tuning and 1,500 operations hours. The implementation of one of eleven lines took about nine months. The authors reported a 10 percent increase in OEE, a 50 percent increase in output and an estimated payback of about 18 months. Those figures describe one implementation. They are useful because they expose labor that a simple license price misses, not because they define a market benchmark.
A NIST MEP case about Enviro Tech reported a USD 29,500 investment and USD 421,450 in stated savings after PLC, ERP and QMS integration. Again, this is a company success story. A buyer should examine the baseline, scope and attribution before using the result in a forecast.
The safest cost model uses plant data. Count assets by interface type. Estimate engineering hours for each machine family. Define the retention period and frequency for every data class. Separate pilot cost from the repeatable cost of the second, tenth and hundredth connection. This reveals whether the architecture becomes cheaper to scale or merely repeats custom work.
Which IIoT architecture should a manufacturer choose
Edge is appropriate when the process needs low latency, local continuity or a reduced data stream. Cloud is useful for scalable computing, multi-site access and managed services. On-premises systems give the plant more direct control but require local infrastructure and skills. Many manufacturers need a hybrid design.
| Criterion | Edge | On premises platform | Cloud platform | Hybrid |
|---|---|---|---|---|
| Response time | Very short | Short on local network | Depends on connection | Short locally, scalable centrally |
| Operation during WAN outage | Strong if designed for it | Strong | Limited without buffering | Strong for critical functions |
| Multi-site analytics | Limited alone | Requires central design | Strong | Strong |
| Data governance | Local control | Direct organizational control | Shared with provider controls | Data classified by purpose |
| Internal support need | Controls and edge skills | Infrastructure and application skills | Integration and vendor management | Broadest skill mix |
| Best fit | Filtering, local logic, buffering | Regulated or tightly controlled local workloads | Cross-site services and elastic analytics | Plants with mixed latency and scale needs |
Architecture should follow the decision. A high-speed quality control loop should not depend on an internet round trip. A monthly comparison of energy intensity across ten plants does not need to run inside each PLC. The system should also define what happens when a connection, model or enterprise application fails. A dashboard that silently stops receiving data can be more dangerous than a visible alarm.
Brownfield plants need an explicit integration policy. OPC UA can reduce proprietary coupling when supported correctly, but it does not make inconsistent tag names or undocumented equipment disappear. The team should create a common asset hierarchy, naming rules, units and timestamps before scaling.
How should a brownfield IIoT pilot be planned
A good brownfield pilot covers one line or asset group, one measurable loss, a documented baseline, an owner of the resulting decision and a written rule for scaling. It should be large enough to test real integration but small enough to stop without trapping the plant in a platform.
- Define the business problem. Use a loss such as unplanned stops, excessive energy per good unit, missing traceability or delayed quality response. Avoid a goal such as “collect more data.”
- Define the decision. State who will use the information, how often and what action becomes possible. If nobody owns the response, an alert is only a notification.
- Build an asset and protocol inventory. Record controller model, network, available tags, documentation quality, machine warranty and change-control restrictions.
- Establish a baseline. Measure the current loss with a stable definition. Include product mix, shift and operating conditions.
- Design the minimum data path. Select only the tags and context required for the use case. Specify units, timestamps, quality flags and retention.
- Perform an OT security review. Define zones, conduits, accounts, encryption where appropriate, remote access, logging, patching and recovery.
- Write acceptance criteria. Examples include data completeness, timestamp accuracy, maximum delay, availability, alert precision and a verified workflow response.
- Run the pilot through normal variability. Include changeovers, network interruptions, maintenance work and the most difficult product variant.
- Measure the result against the baseline. Separate operational change from seasonal demand or unrelated improvement work.
- Decide whether to scale, redesign or stop. Record repeatable connection cost, remaining custom work and the expected value of the next deployment.
This sequence also creates evidence for a broader manufacturing digital transformation roadmap. It prevents a pilot from becoming a permanent demonstration with no route to operating ownership.
What are the main IIoT implementation risks
The main risks are weak business ownership, inconsistent data, uncontrolled links between OT and IT, underestimated integration work and dependence on proprietary components. These risks can exist even when every sensor works.
Industrial environments have availability and safety constraints that differ from office IT. The NIST Guide to Operational Technology Security recommends treating OT according to its performance, reliability and safety requirements. In practice, that means controlled remote access, least privilege, network segmentation, asset inventory, logging, backup and tested recovery. A supplier VPN account left open indefinitely is not an operating model.
Data quality is another operational risk. A model may be mathematically sound but wrong because a sensor was moved, a unit changed or a PLC program was revised. Each important data point needs an owner, a quality rule and change history. Maintenance and controls teams must know which modifications require revalidation.
Vendor lock-in deserves a commercial test. Ask whether data can be exported with timestamps and context, whether interfaces are documented, how pricing changes with tag volume, who owns derived data and what happens at contract termination. A technically successful pilot can still create an expensive dependency.
When does an industrial IoT project pay off
An IIoT project pays off when the value of improved decisions exceeds the full cost of collecting, contextualizing, securing and maintaining the data. The calculation should be tied to an operational baseline rather than a generic percentage improvement.
For a downtime use case, annual gross benefit can be estimated as avoided constraint hours multiplied by contribution per constraint hour. From that amount, subtract added maintenance, platform fees, support labor and the expected cost of false alerts or missed events. For energy, use reduced consumption per good unit at the applicable tariff and production volume. Do not multiply a plant-wide loss by a pilot improvement unless the same cause and architecture genuinely scale.
The business case should include downside sensitivity. Test lower adoption, weaker detection, a longer commissioning period and higher internal labor. Use the same decision rules described in how to evaluate an industrial investment project.
IIoT also creates options. A standard data layer may reduce the cost of later quality, maintenance or planning applications. That option has value, but it should be documented rather than used as an unlimited “strategic benefit.” The next use case should identify which shared assets it reuses and what incremental cost remains.
What does an experienced manufacturer say about integration
Integration produces value when data reaches the operating workflow and reduces a defined source of error.
“The integration of real-time data between our PLC system, ERP, and QMS has significantly reduced human error in our manufacturing processes.”
Brey Funkhouser, Continuous Improvement Manager at Enviro Tech Chemical Services, made this comment in the NIST MEP case study. It supports a specific traceability case. It does not prove that every three-system integration will achieve the same result.
Manufacturers deciding where MES and ERP belong in this flow can use InduVista’s explanation of the difference between MES and ERP. The relevant question is which system owns each record and action, not which application can technically display the tag.
Industrial IoT implementation checklist
- Name the production loss in money, time, quality or risk.
- Identify the decision that better data will change.
- Assign an operational owner and a technical owner.
- Inventory assets, controllers, protocols and existing documentation.
- Define the minimum tags, context, units and frequency.
- Select edge, on-premises and cloud functions by latency and continuity need.
- Complete an OT cybersecurity and remote-access review.
- Price hardware, integration, platform, internal labor and recurring support.
- Write measurable data and workflow acceptance criteria.
- Test normal variability, failures and recovery.
- Compare the result with a documented baseline.
- Record the repeatable cost and evidence required before scaling.
Frequently asked questions
Can industrial IoT be added to legacy machines
Yes. Legacy machines can often be connected through controller interfaces, protocol converters, gateways or retrofit sensors. The right method depends on documentation, warranty, safety, available signals and whether the added measurement represents the process accurately.
Does industrial IoT require cloud computing
No. IIoT can run at the edge or on premises. Cloud services are useful for multi-site access and scalable analytics, but critical local functions should be designed around latency, connectivity and recovery requirements.
What data should an IIoT pilot collect first
Collect only the data needed to describe the selected loss and decision. That normally includes asset state, timestamps, production context, the relevant process variables and an outcome such as good units, downtime or energy use.
How long does an IIoT implementation take
There is no standard duration. A limited pilot may take weeks or months, while a brownfield program across many machine families can take much longer. Protocol access, production availability, security approval and data-context work often determine the schedule.
Sources
- A Survey on Industrial Internet of Things A Cyber Physical Systems Perspective, NIST and IEEE Access, 2018.
- Industrial Internet Reference Architecture, Industry IoT Consortium.
- Guide to Operational Technology Security, NIST SP 800-82 Revision 3, 2023.
- OPC Unified Architecture Overview and Concepts, OPC Foundation.
- Integrating Automation to Enhance Quality Traceability and Efficiency, NIST MEP, 2024.
- Industrial Internet of Things Enabled Kata Methodology, Processes, 2024.

[…] return, management needs a staged commitment or better evidence. For a fuller capital review, use industrial IoT architecture and implementation costs; for lifecycle comparison, use a manufacturing digital transformation […]
[…] Choose the simplest architecture that can support the decision and cybersecurity requirements. An industrial IoT implementation should start with a costly problem and limited pilot, not a plant-wide technology […]
[…] Test a downside case. Reduce adoption, performance and volume. Extend ramp-up. Increase support cost. If a small change destroys the return, management needs a staged commitment or better evidence. For a fuller capital review, use the practical difference between MES and ERP; for lifecycle comparison, use industrial IoT architecture and implementation costs. […]
[…] supporting industrial IoT architecture may be shared with other use cases, but only the genuinely reusable portion belongs to a […]